
Milk Processing Plant Manufacturers in India
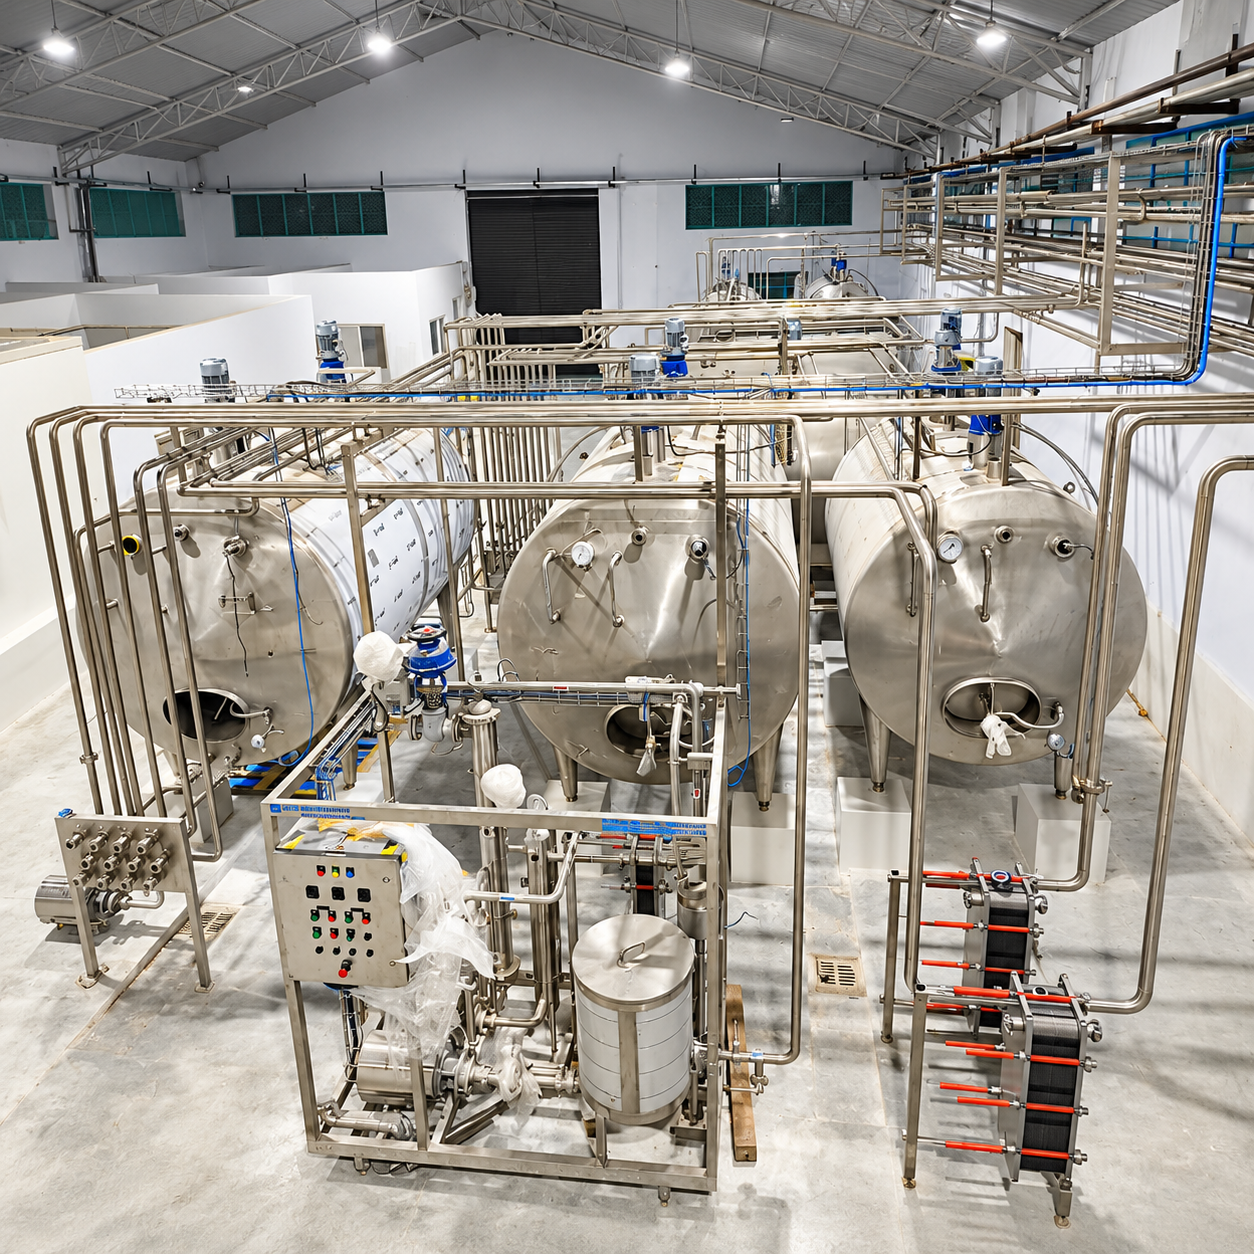
VRS Industries is leading Milk Processing Plant Manufacturers, Suppliers and Dealers in India. With 10+ years of industry experience, we design and manufacture reliable Milk Processing Plant solutions focused on quality, efficient operation, competitive pricing, and long-term performance.
Our capabilities cover customized dairy processing equipment, process automation, CIP systems, chilling, pasteurization, homogenization, storage, and complete plant solutions. We understand that every dairy business has different production needs, so we provide practical engineering solutions designed around capacity, product requirements, and available space.
With experienced technical teams and a strong commitment to timely delivery, we help customers build efficient and dependable dairy processing facilities.
What Is a Milk Processing Plant and How Does It Support Modern Dairy Production?
A Milk Processing Plant is an integrated industrial setup used to receive, chill, process, standardize, pasteurize, homogenize, store, and pack milk for safe commercial distribution. It combines specialized equipment and controlled processing stages to maintain milk quality and consistency. Modern dairy businesses rely on efficient milk processing systems to improve hygiene, productivity, product uniformity, and operational control.
Working Process of Milk Processing Plant
As Milk Processing Plant Manufacturers in India, we provide systematically designed milk processing solutions that cover every stage from hygienic milk reception and chilling to processing, packaging, storage, and dispatch.
- Milk Collection & Reception: Fresh milk is collected, transported hygienically, and tested for quality before processing.
- Filtration & Chilling: Milk is filtered to remove impurities and rapidly chilled to preserve freshness.
- Separation & Standardization: Cream is separated and blended with skim milk to achieve the required fat and SNF levels.
- Pasteurization: Milk is heat-treated under controlled conditions to reduce harmful microorganisms and then cooled quickly.
- Homogenization: High-pressure processing evenly distributes fat particles for a smooth and uniform milk texture.
- Value-Added Processing: Processed milk can be used to manufacture curd, paneer, butter, cheese, ghee, and other dairy products.
- Packaging: Finished milk is hygienically filled into pouches, bottles, or cartons for safe distribution.
- Cold Storage: Packaged products are stored under controlled temperatures to maintain freshness and quality.
- Cleaning & Hygiene: CIP systems clean processing tanks, pipelines, and equipment to maintain hygienic production.
- Quality Control & Dispatch: Final products are checked for quality before being safely stored and dispatched to the market.
Types of Milk Processing Plants
As Milk Processing Plant Suppliers in India, we offer a comprehensive range of processing plants engineered for different capacities, dairy products, processing requirements, and production applications.
- Milk Chilling Plant: This plant collects fresh raw milk from farms and collection centers and rapidly cools it to preserve freshness. It keeps the milk at a controlled temperature for safe storage and transportation to larger dairy facilities.
- Market Milk Plant: It processes raw milk through chilling, pasteurization, homogenization, and packaging. It produces safe, consistent, and ready-to-consume milk for retail and commercial distribution.
- Composite Milk Processing Plant: This plant handles large quantities of milk and supports multiple dairy processing operations. It can produce market milk as well as value-added products such as butter, cheese, ghee, and milk powder.
- Pasteurization Plant: It uses controlled heat treatment to reduce harmful microorganisms in milk. The process helps improve milk safety while retaining its desired quality, taste, and nutritional properties.
- UHT Milk Processing Plant: A UHT plant heats milk to a very high temperature for a short period under controlled conditions. It helps provide extended shelf life when the treated milk is packed using suitable aseptic packaging technology.
- Homogenization Plant: It processes milk under high pressure to break down fat globules into smaller, evenly distributed particles. This helps prevent cream separation and provides milk with a smooth and uniform consistency.
- Yogurt & Curd Processing Plant: This plant is designed for controlled fermentation and processing of milk into yogurt, curd, lassi, and similar cultured dairy products. It provides controlled processing conditions to achieve consistent texture, taste, and product quality.
- Cheese Processing Plant: It converts milk into different types of cheese through controlled coagulation, cutting, draining, pressing, and related processes. The equipment configuration can be selected according to the required cheese variety and production capacity.
- Butter & Ghee Processing Plant: These plants are designed to process milk or cream into butter and ghee through specialized separation and heating operations. They provide controlled processing conditions for consistent product quality and efficient production.
- Condensed Milk Plant: It removes a controlled amount of water from milk to produce a concentrated dairy product. Vacuum-based evaporation helps achieve the required concentration while supporting efficient and controlled processing.
- Milk Powder Plant: It removes moisture from processed milk through evaporation and spray drying. The resulting powder offers convenient handling, storage, transportation, and extended usability.
- Turnkey Milk Processing Plant: A turnkey plant provides a complete dairy processing solution from initial plant design and equipment selection to fabrication and installation. It can also include automation, commissioning, testing, and project support according to specific production requirements.
Key Features and Benefits of a Milk Processing Plant
As Milk Processing Plant Dealers in India, we deliver modern dairy processing systems equipped with hygienic construction, process automation, efficient equipment, and integrated technologies for reliable and economical operation.
| Key Feature | Primary Benefit | Technical Advantage | Business Value |
|---|---|---|---|
| Hygienic Stainless-Steel Construction | Supports safe and hygienic milk processing. | Sanitary stainless-steel product-contact surfaces are easy to clean and maintain. | Helps maintain consistent product quality and meet hygiene requirements. |
| Automated Process Control | Provides precise control over critical processing operations. | PLC-based systems can monitor and control temperature, flow, pressure, and other process parameters. | Reduces manual intervention, minimizes process variation, and improves productivity. |
| Efficient Pasteurization System | Helps ensure microbiologically safer milk. | Controlled heating followed by rapid cooling provides consistent pasteurization conditions. | Supports reliable production of high-quality processed milk with consistent results. |
| High-Pressure Homogenization | Produces smooth and uniform milk consistency. | Breaks down and disperses fat globules to reduce cream separation. | Improves product appearance, texture, stability, and consumer acceptance. |
| Modular Plant Design | Enables the plant to be configured according to production needs. | Processing units, tanks, pipelines, and equipment can be arranged based on capacity and available space. | Simplifies future expansion, upgrades, and capacity enhancement. |
| Integrated CIP (Clean-in-Place) System | Improves cleaning efficiency and plant hygiene. | Cleaning solutions are automatically circulated through tanks, pipelines, and processing equipment. | Reduces cleaning time and labor requirements while supporting hygienic operations. |
| Energy-Efficient Processing Equipment | Optimizes energy and utility consumption. | Efficient heat exchangers, pumps, and processing systems help minimize unnecessary energy use. | Helps reduce operating costs and improve long-term plant profitability. |
Applications of Milk Processing Plant
As Milk Processing Plant Supplier in India, we provide versatile dairy processing solutions suitable for milk collection, chilling, pasteurization, homogenization, value-added product manufacturing, and complete commercial dairy production.
- Packaged Milk Production: A Dairy Milk Processing Plant is widely used to process, standardize, pasteurize, homogenize, and package milk for hygienic retail and commercial distribution.
- Milk Chilling & Collection: A Mini Milk Processing Plant can support milk collection centers by rapidly chilling and safely storing fresh milk before transportation to larger dairy facilities.
- Pasteurized Milk Manufacturing: A milk Pasteurization processing plant is used to produce safe, fresh, and consistent pasteurized milk for daily consumer and institutional requirements.
- Homogenized Milk Production: A milk Homogenization processing plant helps produce smooth and uniform milk by evenly distributing fat particles throughout the product.
- Value-Added Dairy Products: An Integrated Milk Processing Plant can support the production of curd, yogurt, paneer, butter, ghee, cream, cheese, and other milk-based products.
- Commercial Dairy Production: An automatic milk processing plant helps medium and large dairy businesses manage continuous processing with improved production control and reduced manual intervention.
- Milk Powder & Concentrated Products: An industrial milk processing plant can be integrated with evaporation and drying systems for manufacturing condensed milk and milk powder.
- Complete Dairy Production Projects: A turnkey milk processing plant is suitable for businesses seeking an end-to-end solution covering processing equipment, plant integration, automation, installation, and commissioning, including an Integrated Milk Processing Plant Machine for streamlined processing operations.
Why Choose Us?
- 10+ Years of Industry Experience: We bring over a decade of experience in designing and supplying reliable dairy processing solutions tailored to different production requirements.
- Quality with Competitive Pricing: We combine quality-focused manufacturing, efficient engineering, and competitive pricing to deliver dependable processing equipment with strong long-term value.
- Customized End-to-End Solutions: We provide customized plant solutions with suitable equipment, process integration, automation, installation, and technical support to help ensure smooth and efficient dairy operations.
Choose VRS Industries is trusted Milk Processing Plant Manufacturers, Suppliers and Dealers in India. We provide reliable and customized Milk Processing Plant solutions designed for efficient, hygienic, and consistent dairy production. With 10+ years of experience, strong technical capabilities, quality-focused manufacturing, and competitive pricing, we help dairy businesses develop practical processing facilities suited to their specific production and growth requirements.
FAQ’s
Common equipment includes milk reception systems, storage tanks, milk chillers, clarifiers, separators, pasteurizers, homogenizers, CIP systems, pipelines, and packaging machines. The equipment selection depends on plant capacity and product requirements.
Pasteurization uses controlled heat treatment to reduce harmful microorganisms present in milk. It improves product safety while helping maintain the desired taste and quality of milk.
Yes, a suitably designed plant can support products such as packaged milk, curd, yogurt, paneer, butter, cream, cheese, ghee, and milk powder. The required equipment and process configuration vary according to the product.
Homogenization breaks milk fat globules into smaller and evenly distributed particles. This helps prevent cream separation and provides milk with a smooth, uniform consistency.