
Beverage Processing Plant Manufacturers in Pune
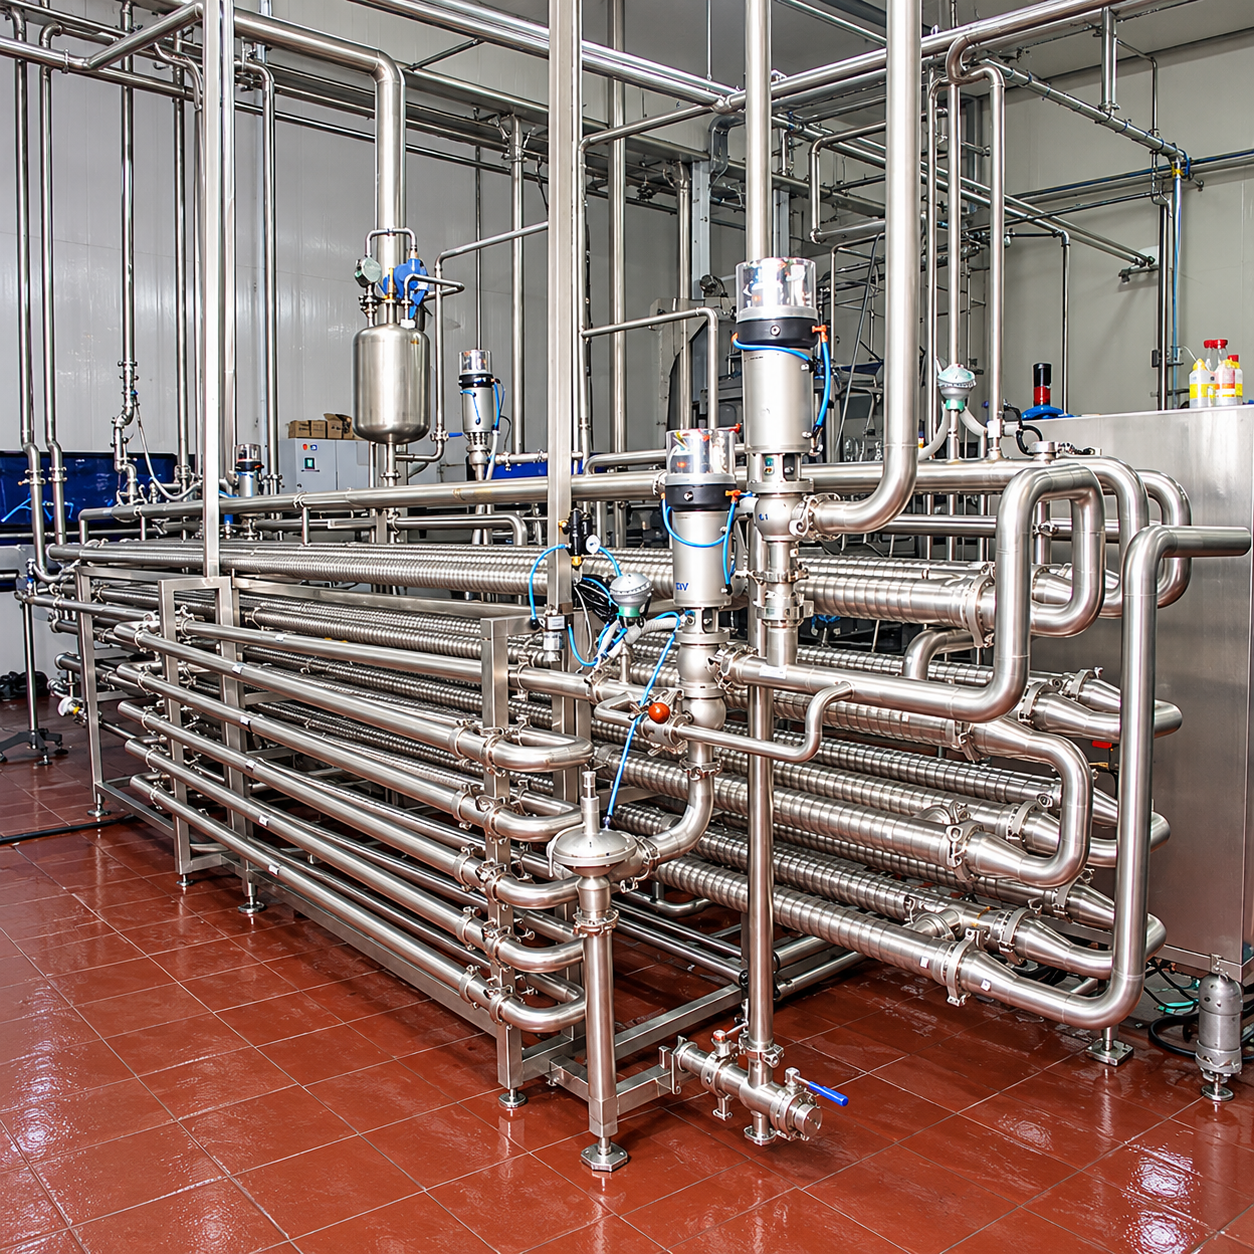
VRS Industries is trusted Beverage Processing Plant Manufacturers, Suppliers and Dealers in Pune. Having 10+ years of industry experience, we provide complete beverage processing solutions designed to meet the changing needs of beverage manufacturers.
With our expertise in process engineering, precision fabrication, automation, and project execution, we develop systems that deliver reliable performance and consistent product quality. We prioritize hygienic construction, efficient operation, competitive pricing, and easy maintenance in every project we undertake.
From beverage preparation, blending, filtration, and heat treatment to homogenization and CIP integration, we offer customized solutions based on product requirements and production capacity. Our experienced team supports every stage, helping customers achieve smooth, scalable, and cost-effective beverage production.
What Is a Beverage Processing Plant and Why Is It Essential for Efficient Production?
A beverage processing plant is an integrated production facility designed to prepare, process, treat, and transfer beverages before filling and packaging. It brings together hygienic tanks, pumps, heat exchangers, filtration units, piping, automation, and cleaning systems for smooth operation. Modern beverage processing equipment helps manufacturers maintain consistent product quality, improve hygiene, optimize production efficiency, and meet the processing requirements of different beverage types and capacities.
Working Process of a Beverage Processing Plant
As Beverage Processing Plant Manufacturers in Pune, we follow a systematic processing approach that ensures hygienic handling, consistent quality, and efficient beverage production at every stage.
- Raw Material Preparation: We begin by receiving, inspecting, measuring, and preparing the required ingredients before hygienically transferring them into the processing system.
- Ingredient Mixing & Blending: Water, sugar, flavours, concentrates, and other ingredients are carefully combined to achieve the desired recipe, taste, and product consistency.
- Filtration & Deaeration: The prepared beverage passes through filtration and, where required, deaeration to improve product clarity and minimize unwanted dissolved air.
- Pasteurization or Sterilization: We apply controlled heat treatment according to the product requirements to support beverage safety, quality, and storage stability.
- Homogenization: For beverages such as flavoured milk, homogenization creates a more uniform product by reducing particle size and improving texture and stability.
- Hygienic Product Transfer: Sanitary pumps, valves, and stainless-steel pipelines move the processed beverage smoothly between tanks and connected processing equipment.
- Filling & Packaging: Once processing is complete, the finished beverage is supplied to the filling section for accurate filling, sealing, and packaging in the selected containers.
- CIP Cleaning: Clean-in-Place procedures clean tanks, pipelines, heat exchangers, and other product-contact surfaces, helping maintain hygienic conditions and production readiness.
This integrated beverage processing line helps manufacturers achieve controlled processing, repeatable quality, hygienic operation, and efficient movement of beverages from raw materials to the filling stage.
Types of Beverage Processing Plants
As Beverage Processing Plant Suppliers in Pune, we offer versatile plant solutions designed to meet the specific processing, capacity, and product requirements of different beverage industries.
- Fruit Juice & Pulp Processing Plant: Designed for fruit washing, pulping, extraction, filtration, blending, and pasteurization. It supports efficient processing of juices, purees, and concentrates with consistent quality.
- Carbonated Soft Drink Processing Plant: Used for water treatment, syrup blending, chilling, and controlled CO₂ carbonation. It helps maintain uniform taste, carbonation, and product quality.
- Dairy & Plant-Based Milk Processing Plant: Suitable for milk, flavoured milk, whey drinks, and plant-based beverages. Homogenization and heat treatment help achieve smooth texture, stability, and hygiene.
- Ready-to-Drink & Functional Beverage Plant: Processes energy drinks, sports drinks, iced teas, coffee beverages, and functional formulations. Accurate mixing and automated control ensure consistent formulation and production.
- Alcoholic Beverage Processing Plant: Designed for beer, wine, spirits, and other fermented or distilled beverages. It can incorporate fermentation, filtration, distillation, and storage processes as required.
- Flavoured Milk Processing Plant: Combines ingredient blending, homogenization, pasteurization, and hygienic product handling. It delivers uniform flavour, smooth consistency, and reliable processing performance.
- Energy Beverage Processing Plant: Designed for accurate formulation, blending, filtration, and controlled heat processing of energy drinks. Automation helps maintain recipe accuracy and consistent production quality.
- Aerated Water Processing Plant: Used for hygienic water treatment and controlled carbonation of aerated water products. It supports clean processing, consistent carbonation, and efficient production.
Features & Benefits of Beverage Processing Plant
As Beverage Processing Plant Dealers in Pune, we provide carefully engineered solutions that combine hygienic construction, process efficiency, automation, flexibility, and dependable performance.
| Key Feature | How It Works | Key Benefit | Business Value |
|---|---|---|---|
| Hygienic Stainless-Steel Construction | Uses food-grade stainless steel for product-contact surfaces. | Better Hygiene | Supports safe and consistent beverage processing. |
| Customized Plant Design | Designed according to beverage type, capacity, and layout. | Flexible Processing | Meets specific production requirements efficiently. |
| Advanced Process Automation | Controls key processing parameters with minimal manual intervention. | Accurate Operation | Improves process consistency and productivity. |
| Efficient Process Integration | Connects different processing stages into a coordinated system. | Smooth Production Flow | Reduces interruptions and improves operational efficiency. |
| CIP-Compatible System | Facilitates systematic cleaning of tanks, pipelines, and equipment. | Easy Cleaning | Supports consistent sanitation and reduced cleaning effort. |
| Precise Temperature Control | Maintains required temperatures during critical processing stages. | Consistent Quality | Helps achieve uniform beverage quality and stability. |
| Modular & Scalable Configuration | Allows convenient installation, maintenance, and future expansion. | Greater Flexibility | Supports changing production needs and capacity growth. |
As Beverage Processing Plant Suppliers in Pune, we focus on delivering efficient and adaptable solutions that help beverage manufacturers achieve reliable production, consistent quality, easy maintenance, and long-term operational value.
Applications of Beverage Processing Plant
As Beverage Processing Plant Manufacturers in Pune, we deliver versatile processing solutions suitable for a wide range of beverage applications, from juices and soft drinks to dairy, functional, and ready-to-drink products.
- Commercial Juice Processing: Used for efficient extraction, pulping, clarification, concentration, and heat treatment of fruit juices while supporting hygienic and consistent production.
- Fruit Beverage Manufacturing: Suitable for producing ready-to-serve juices, nectars, and blended beverages made from mango, orange, apple, mixed fruits, and similar formulations.
- Carbonated Soft Drink Production: Supports water treatment, syrup preparation, blending, cooling, and controlled carbonation for consistent sparkling beverage production.
- Dairy & Plant-Based Beverages: Designed for processing flavoured milk, whey drinks, coconut milk, soy milk, almond milk, and other dairy or plant-based beverages with suitable homogenization and heat treatment.
- Functional & Health Beverages: Suitable for producing energy drinks, functional waters, herbal beverages, and vitamin-enriched formulations with controlled ingredient blending and processing.
- Packaged Drinking Water: Can be integrated with suitable water purification stages such as RO, UV, and ozone treatment for hygienic packaged water production.
- Ready-to-Drink Beverage Production: Supports the preparation and processing of iced teas, coffee drinks, sports beverages, and other convenient ready-to-consume products.
- Multi-Product Beverage Processing: A flexible beverage processing system can be configured for different formulations, helping manufacturers achieve efficient production and consistent product quality.
Why Choose Us?
- Customized Process Solutions: We develop each beverage production plant according to the product type, required capacity, available space, and specific production needs.
- Quality-Driven Engineering: We focus on hygienic construction, dependable components, and accurate process control to deliver consistent performance and reliable beverage production.
- Complete Project Support: We manage every stage from process design and fabrication to installation, commissioning, and technical support for a smooth project experience.
Choose VRS Industries is well-known Beverage Processing Plant Manufacturers, Suppliers and Dealers in Pune. We deliver customized beverage processing solutions that combine quality engineering, hygienic design, efficient operation, and dependable performance. With our technical expertise and customer-focused approach, we help beverage manufacturers establish reliable production facilities designed for consistent output, easy maintenance, and sustainable business growth. Connect with us for additional details.
FAQ’s
The plant can be designed for juices, soft drinks, flavoured milk, energy drinks, RTD beverages, plant-based drinks, and aerated water. The configuration depends on the product formulation and process requirements.
The process generally includes ingredient preparation, mixing, filtration, heat treatment, homogenization, product transfer, and filling. CIP cleaning is also incorporated to maintain hygienic processing conditions.
Plant capacity varies according to the product, processing stages, equipment configuration, and production target. A suitable capacity can be selected based on the required hourly or daily output.
Yes, PLC/SCADA-based automation can be incorporated for monitoring and controlling important process parameters. It can improve accuracy, repeatability, and operational efficiency.