
Milk Processing Equipment Manufacturers in India
VRS Industries is prominent Milk Processing Equipment Manufacturers, Suppliers and Dealers in India. With 10+ years of industry experience, we specialize in designing, manufacturing, and supplying advanced industrial milk processing equipment for dairy businesses of varying capacities.
We deliver customized solutions for milk reception, storage, pasteurization, separation, homogenization, cooling, and other dairy processing requirements. By combining high-quality materials, competitive pricing, modern engineering, and application-focused designs, we help businesses achieve hygienic, consistent, and efficient production.
From initial process planning and equipment selection to installation, automation, commissioning, and after-sales support, we provide dependable end-to-end solutions tailored to each customer’s specific needs.
What Is Milk Processing Equipment and Why Is It Important?
Milk Processing Equipment refers to purpose-built machinery used throughout the dairy production process, from receiving and storing raw milk to treating, cooling, and preparing it for final use. These systems help dairy manufacturers maintain hygienic handling, accurate temperature control, uniform product quality, and smooth production flow. They are widely used for producing packaged milk, cream, butter, ghee, paneer, curd, cheese, and various other dairy products while supporting efficient and reliable plant operations.
Working Process of Milk Processing Equipment
As Milk Processing Equipment Manufacturers in India, we provide efficient systems for hygienic milk handling, processing, cooling, and packaging.
- Milk Reception: Fresh milk is received from collection centers or tankers and hygienically transferred into the processing line for initial handling.
- Milk Storage: The collected milk is temporarily stored in hygienic Milk tanks designed to maintain suitable conditions before the next processing stage.
- Filtration & Clarification: The milk passes through filtration and clarification systems to remove unwanted particles and prepare it for further processing.
- Cream Separation: A high-efficiency milk separator separates cream from skimmed milk according to the desired product composition and processing requirements.
- Milk Standardization: The fat and solids content of milk is adjusted to achieve the required formulation and maintain consistent product quality.
- Homogenization: The milk passes through a milk homogenizer under controlled pressure, reducing fat globules and creating a smooth, uniform product.
- Pasteurization: A milk pasteurizer machine applies controlled heat treatment to reduce harmful microorganisms before rapidly cooling the milk to protect its quality.
- Cooling & Storage: After thermal processing, the milk is rapidly cooled using milk cooling equipment and transferred to a hygienic milk storage tank until filling or further processing.
- Filling & Packaging: The finished milk is conveyed to the appropriate packaging system, where it is hygienically filled, sealed, and prepared for distribution.
Types of Milk Processing Equipment
As Milk Processing Equipment Suppliers in India, we offer reliable machinery for efficient milk processing and diverse dairy product applications.
- Milking Machines: Modern milking systems automate milk collection from dairy animals in a controlled and hygienic manner. They reduce manual effort while improving collection speed, cleanliness, and overall milking efficiency, complemented by options like an automatic milking machine for advanced setups.
- Bulk Milk Coolers (BMC) / Chillers: Freshly collected milk is rapidly cooled through BMC units to reach suitable storage conditions. This quick cooling helps limit bacterial growth and preserves milk freshness before further processing.
- Milk Storage Tanks & Silos: Insulated stainless-steel vessels provide hygienic storage for raw or processed milk before the next production stage. They maintain controlled conditions while supporting continuous milk handling and processing.
- Cream Separators: High-speed centrifugal separation divides whole milk into cream and skimmed milk with accuracy. This process allows dairy manufacturers to control fat content and prepare different milk-based products.
- Pasteurizers: Controlled heat treatment reduces undesirable microorganisms in milk while maintaining its required quality and characteristics. Batch and HTST configurations can be selected according to production capacity and processing needs.
- Homogenizers: High-pressure treatment breaks down milk fat globules and distributes them evenly throughout the product. This creates a smoother consistency and helps prevent cream from separating during storage.
- Butter Churners: Mechanical cream agitation separates butterfat from buttermilk and converts cream into fresh butter. Controlled churning supports uniform texture, efficient production, and consistent batch results.
- Ghee Clarifiers: Controlled heating and clarification remove excess moisture and unwanted particles from butter. This produces clear, refined ghee with improved stability and a clean appearance.
- Khoa / Mawa Machines: Continuous heating and scraping concentrate milk by removing moisture and producing a thick khoa or mawa consistency. These systems help manufacturers achieve faster and more uniform production for traditional dairy sweets.
- Paneer & Cheese Vats / Presses: Coagulation and curd-processing stages convert prepared milk into paneer or cheese while controlled cutting and whey drainage support consistent results. Pressing equipment then provides the desired shape, firmness, and texture.
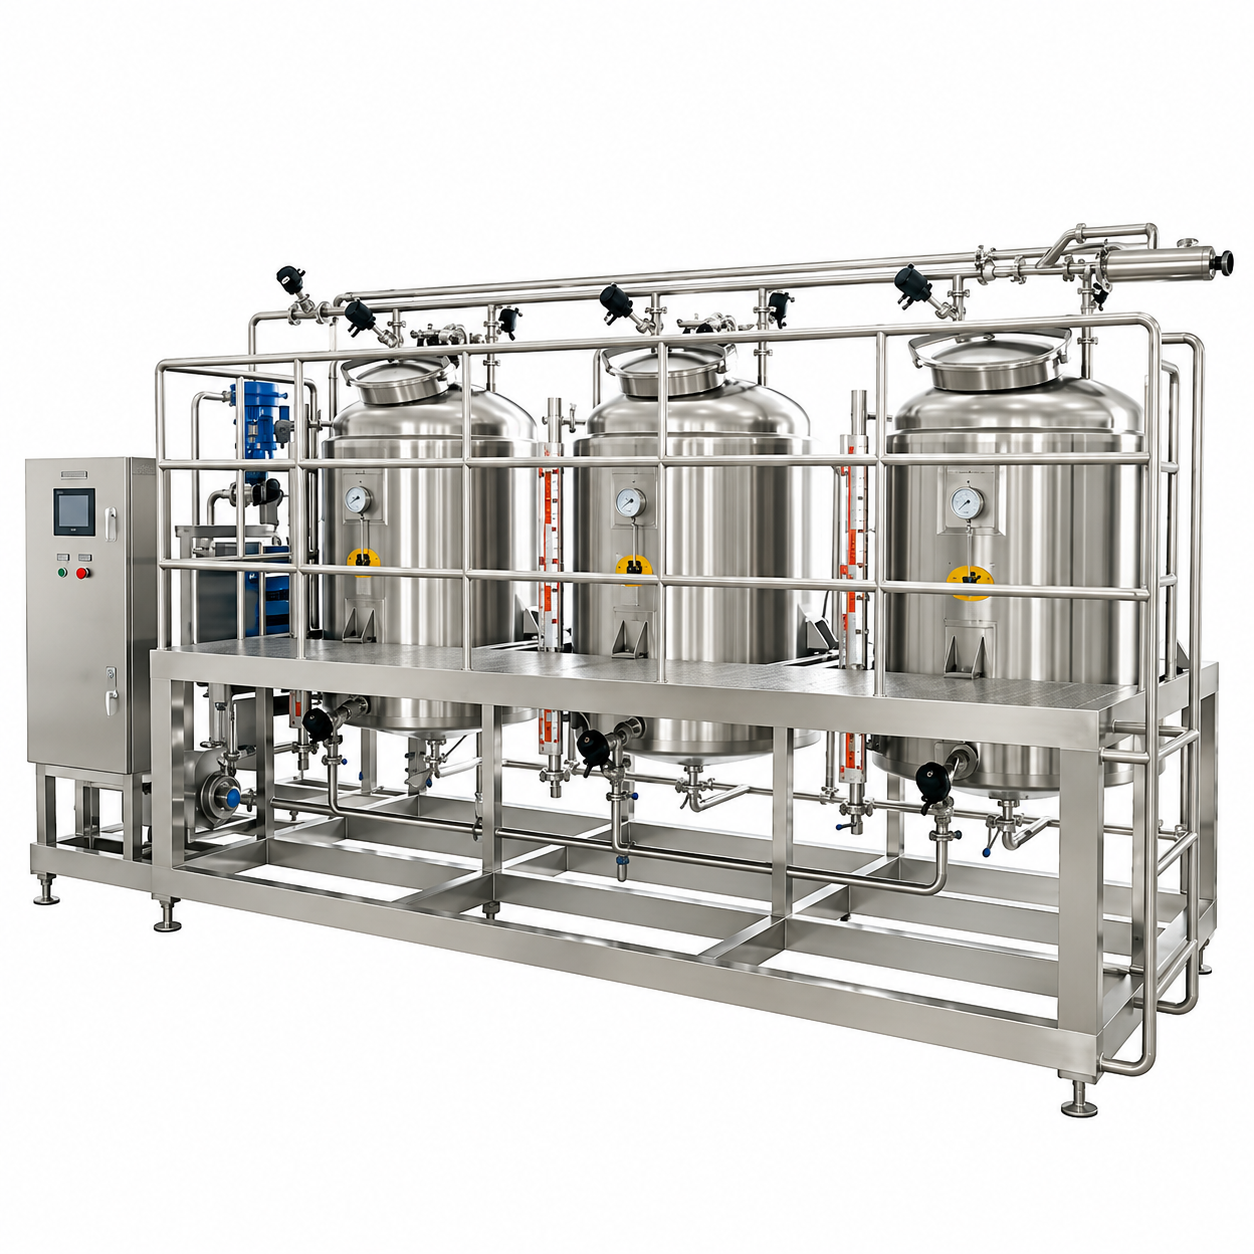
- CIP (Cleaning-in-Place) Systems: Automated circulation of cleaning solutions cleans internal surfaces of tanks, pipelines, vessels, and processing equipment without complete dismantling. These systems support hygienic production while reducing cleaning time and manual intervention.
- Packaging & Filling Machines: Automated filling systems transfer finished milk and dairy products into pouches, bottles, cartons, or other suitable packaging formats. Accurate dosing and hygienic sealing improve production speed and help protect the finished product.
Key Features and Benefits of Milk Processing Equipment
As Milk Processing Equipment Dealers in India, we supply equipment designed for hygienic operation, precise processing, and consistent performance.
| Key Feature | How It Supports Processing | Key Benefit | Business Value |
|---|---|---|---|
| Hygienic Stainless-Steel Design | Food-grade stainless steel ensures clean and durable product-contact surfaces. | Better Hygiene | Supports sanitary processing and consistent milk quality. |
| Automated Process Control | PLCs, sensors, and HMIs control critical processing parameters. | Higher Accuracy | Reduces manual errors and improves process consistency. |
| Custom Capacity Options | Equipment is configured according to production volume and plant requirements. | Production Flexibility | Supports current needs and future capacity expansion. |
| Efficient Heating & Cooling | Controlled systems manage milk heating, cooling, and temperature changes. | Better Efficiency | Helps optimize processing time and utility consumption. |
| Integrated Processing System | Pumps, pipelines, tanks, controls, and equipment work as a connected system. | Smooth Operation | Improves product flow and reduces manual handling. |
| Precision Milk Separation | Centrifugal separators separate cream and skim milk efficiently. | Consistent Composition | Enables accurate fat control for different dairy products. |
| High-Pressure Homogenization | High pressure reduces and evenly distributes milk fat globules. | Uniform Quality | Produces smoother milk with improved stability. |
| Controlled Pasteurization | Automated systems regulate temperature and holding time precisely. | Product Safety | Supports effective microbial reduction and consistent quality. |
| CIP-Compatible Design | Equipment and pipelines support Cleaning-in-Place systems. | Easy Sanitation | Simplifies cleaning and reduces cleaning downtime. |
| Turnkey Project Solutions | Includes equipment, automation, installation, and commissioning. | Complete Solution | Provides a streamlined approach from plant design to operation. |
Applications of Milk Processing Equipment
As Milk Processing Equipment Manufacturers in India, we provide processing solutions for milk production and a wide range of dairy applications.
- Commercial Dairy Milk Production: Our systems support hygienic milk reception, processing, pasteurization, cooling, and packaging for efficient large-scale dairy production, utilizing specialized milk processing machines for every stage.
- Milk Standardization & Cream Separation: Advanced processing lines can use a milk separator to control fat content and prepare standardized milk, cream, and skimmed milk for different products.
- Paneer & Cheese Manufacturing: Integrated dairy systems help prepare milk for coagulation, curd handling, whey separation, and pressing during commercial paneer and cheese production.
- Butter & Ghee Processing: Specialized equipment supports cream processing, butter making, clarification, and controlled heating for consistent production of butter and ghee.
- Curd & Fermented Dairy Products: Controlled heating, cooling, holding, and fermentation stages can be incorporated into a Milk Processing Unit for curd, lassi, and other cultured dairy products.
- Milk Collection & Cold Storage: Milk cooling equipment and hygienic storage systems help maintain suitable conditions for freshly collected milk before it enters the main processing line.
- Concentrated & Powdered Dairy Products: Suitable Milk Processing Machinery can be integrated with evaporation and drying processes for producing concentrated milk products and dairy powders as part of a complete milk production line and equipment arrangement.
- Complete Dairy Plant Operations: Our milk processing plant equipment can be integrated into a comprehensive milk production line and equipment setup covering milk reception, storage, processing, automation, cleaning, and final packaging. For turnkey execution, integrated milk processing plant machine setup delivers seamless operation from raw milk intake to final packaged goods.
Why Choose Us?
- Experienced Dairy Processing Expertise: We bring practical industry knowledge and turnkey project expertise to design dependable milk processing solutions suited to different production requirements.
- Customized & Hygienic Solutions: We develop processing systems with food-grade stainless-steel construction and customized layouts to meet specific capacity, product, hygiene, and operational requirements.
- Complete Project & Technical Support: We manage the complete journey from process engineering and equipment selection to automation, installation, commissioning, operator training, and after-sales technical assistance.
Choose VRS Industries is well-known Milk Processing Equipment Manufacturers, Suppliers and Dealers in India. We help dairy businesses achieve smooth and hygienic production with thoughtfully engineered Milk Processing Equipment. From customized system design to installation and technical support, we focus on dependable performance, efficient processing, and consistent results, delivering solutions that meet present production requirements while providing flexibility for future dairy business expansion. Reach out to us for additional information.
FAQ’s
Homogenization reduces milk fat globules and distributes them more evenly, helping create a smooth, consistent product and minimizing cream separation.
A milk separator uses centrifugal action to separate cream from skimmed milk, making it useful for fat adjustment and the production of different dairy products.
A typical setup may include storage tanks, separators, pasteurizers, homogenizers, cooling systems, processing vessels, CIP systems, and suitable filling and packaging equipment.
Depending on the plant configuration, the equipment can support production of packaged milk, cream, butter, ghee, paneer, curd, cheese, flavored milk, and other value-added dairy products.